
Welcome to Medke
Shenzhen Medke Technology Co., Ltd. is a leading manufacturer of medical accessories and consumables. Established in 2008 with a registered capital of RMB 10 million, Medke is headquartered in the coastal city of Shenzhen — widely regarded as the "Silicon Valley" of China's medical electronics industry.
Over a decade of growth, we have built a complete chain spanning design, R&D, production and sales, delivering one-stop solutions across patient monitoring accessories — SpO2 sensors, ECG/EKG cables, NIBP cuffs, IBP cables, temperature probes, EEG cables, ESU consumables and fetal monitoring probes. Our plants operate under ISO 13485 and our products are certified with TÜV CE and FDA, opening access to major global markets. We provide reliable OEM / ODM services and export to more than 100 countries and regions worldwide.
Our Journey
Medke Technology was established with a registered capital of 1 million RMB and a factory area of 1,000㎡.
The factory area expanded to 2,000㎡, and a 100,000-class cleanroom was put into operation.
Medke obtained the "Medical Device Manufacturing Enterprise License".
The "MEDKE" brand was officially trademarked.
Achieved TÜV ISO 13485:2003 quality management system certification.
The registered capital increased to 10 million RMB.
Medke products passed FDA certification in the United States.
The factory area expanded to 3,000㎡.
Successfully passed TÜV factory quality inspection.
Support comprehensive OEM solutions.
Expanded into online channels, becoming a Gold Supplier on Alibaba.
Completed the upgrade to comply with EU MDR regulations.
Implemented lean production across the entire supply chain.
Established a modern, intelligent production facility spanning over 4,000㎡, integrating R&D and manufacturing capabilities.
Scroll to explore all milestones
Factory at a Glance
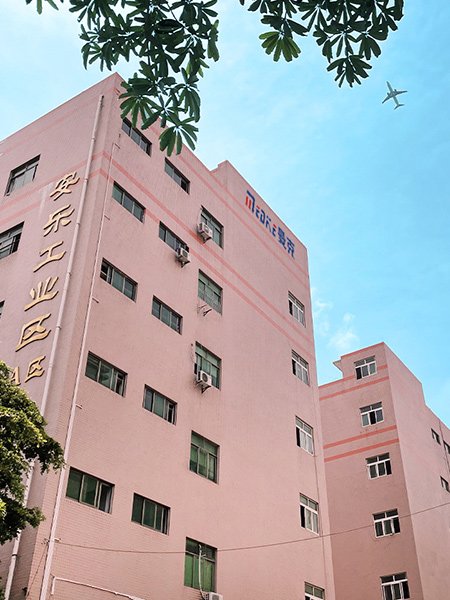
Factory Exterior
4,000㎡ smart factory
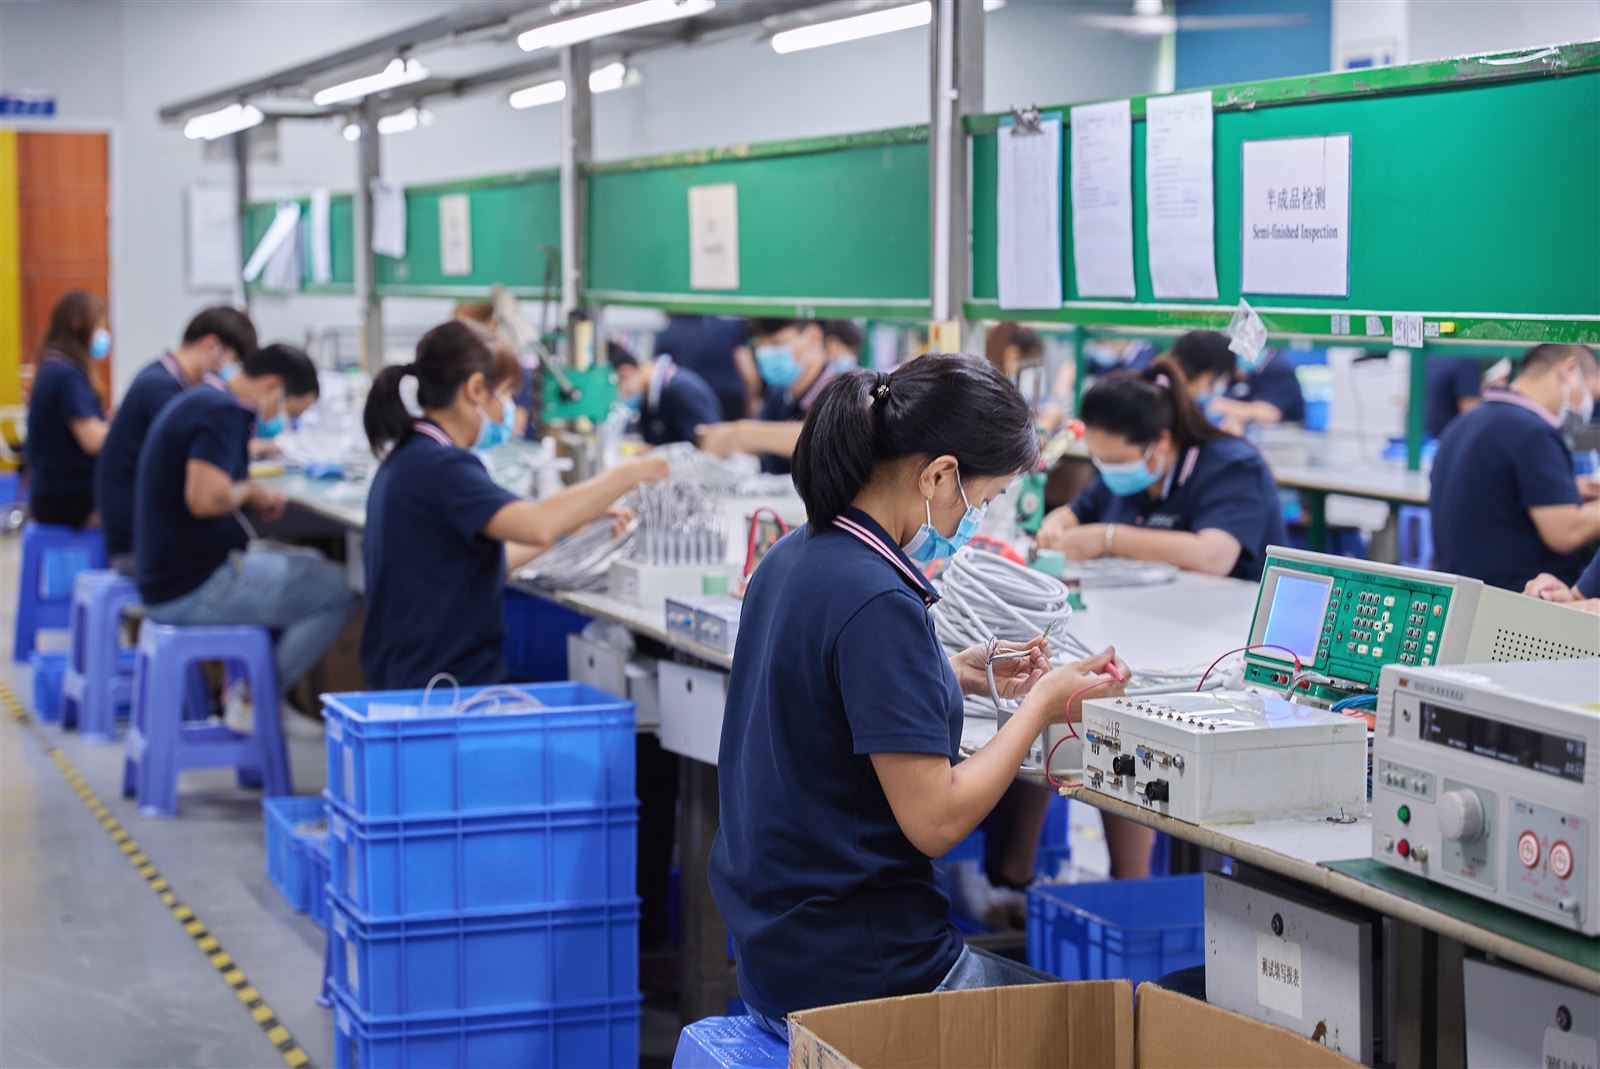
Workshop
Cleanroom workshop
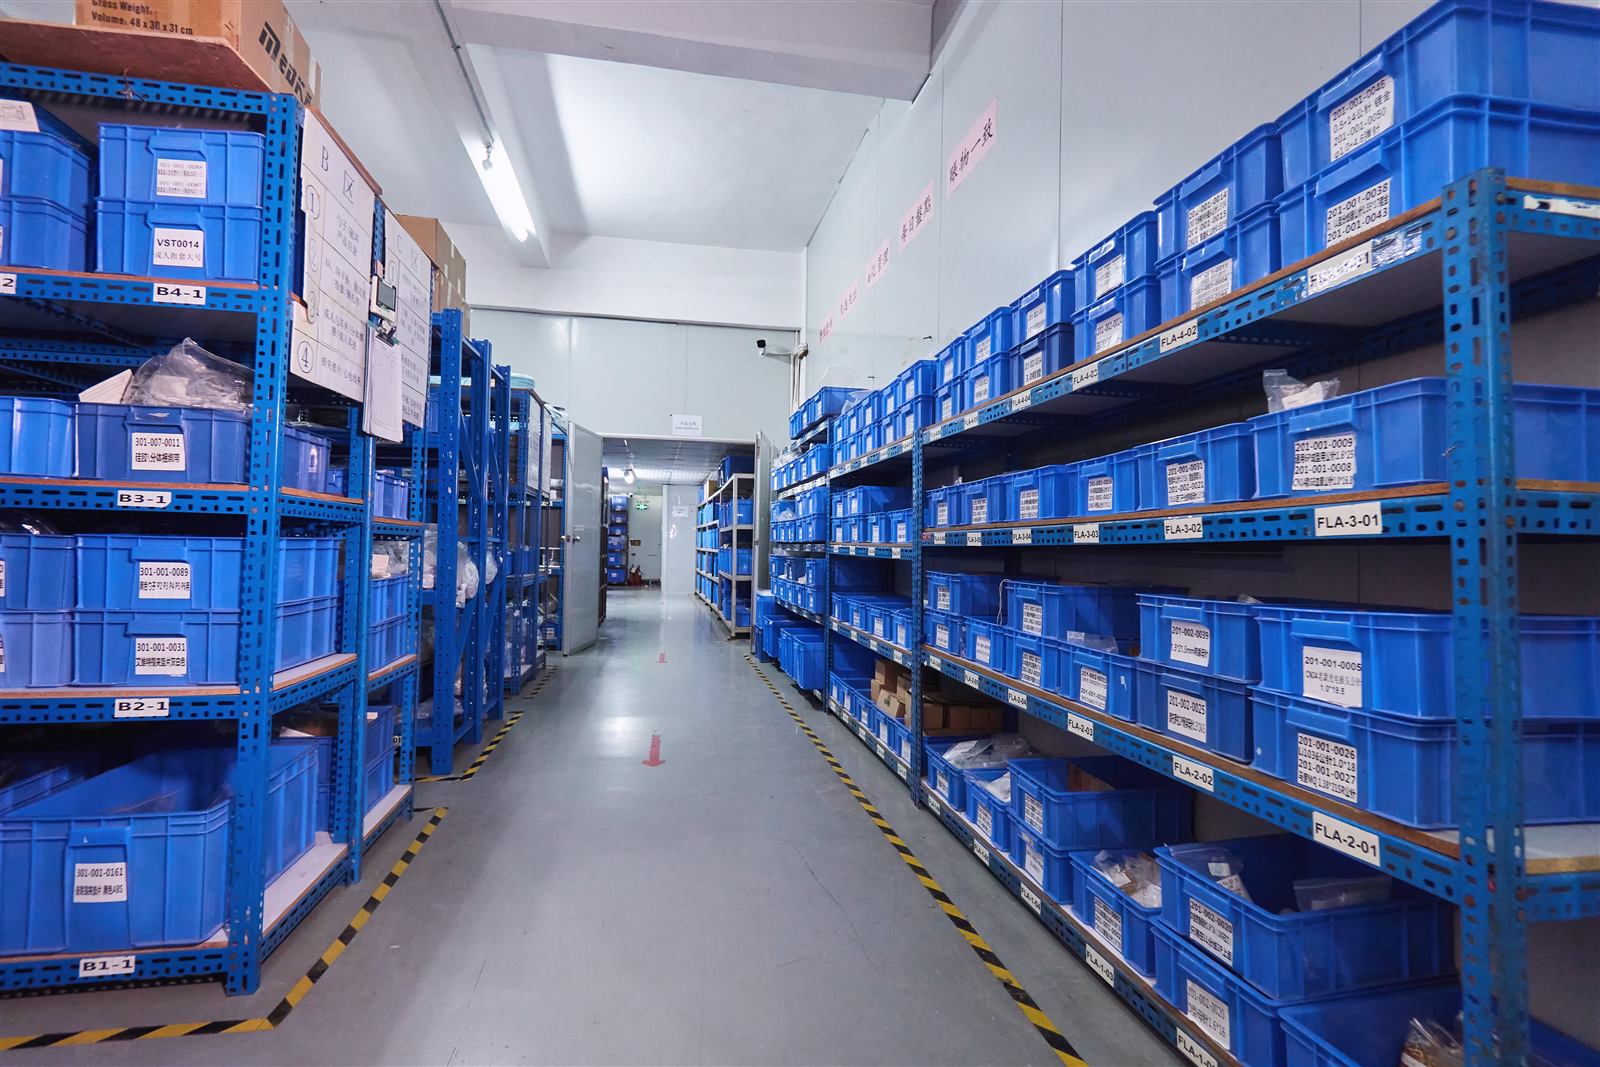
Warehouse
Finished-goods warehouse · fast dispatch
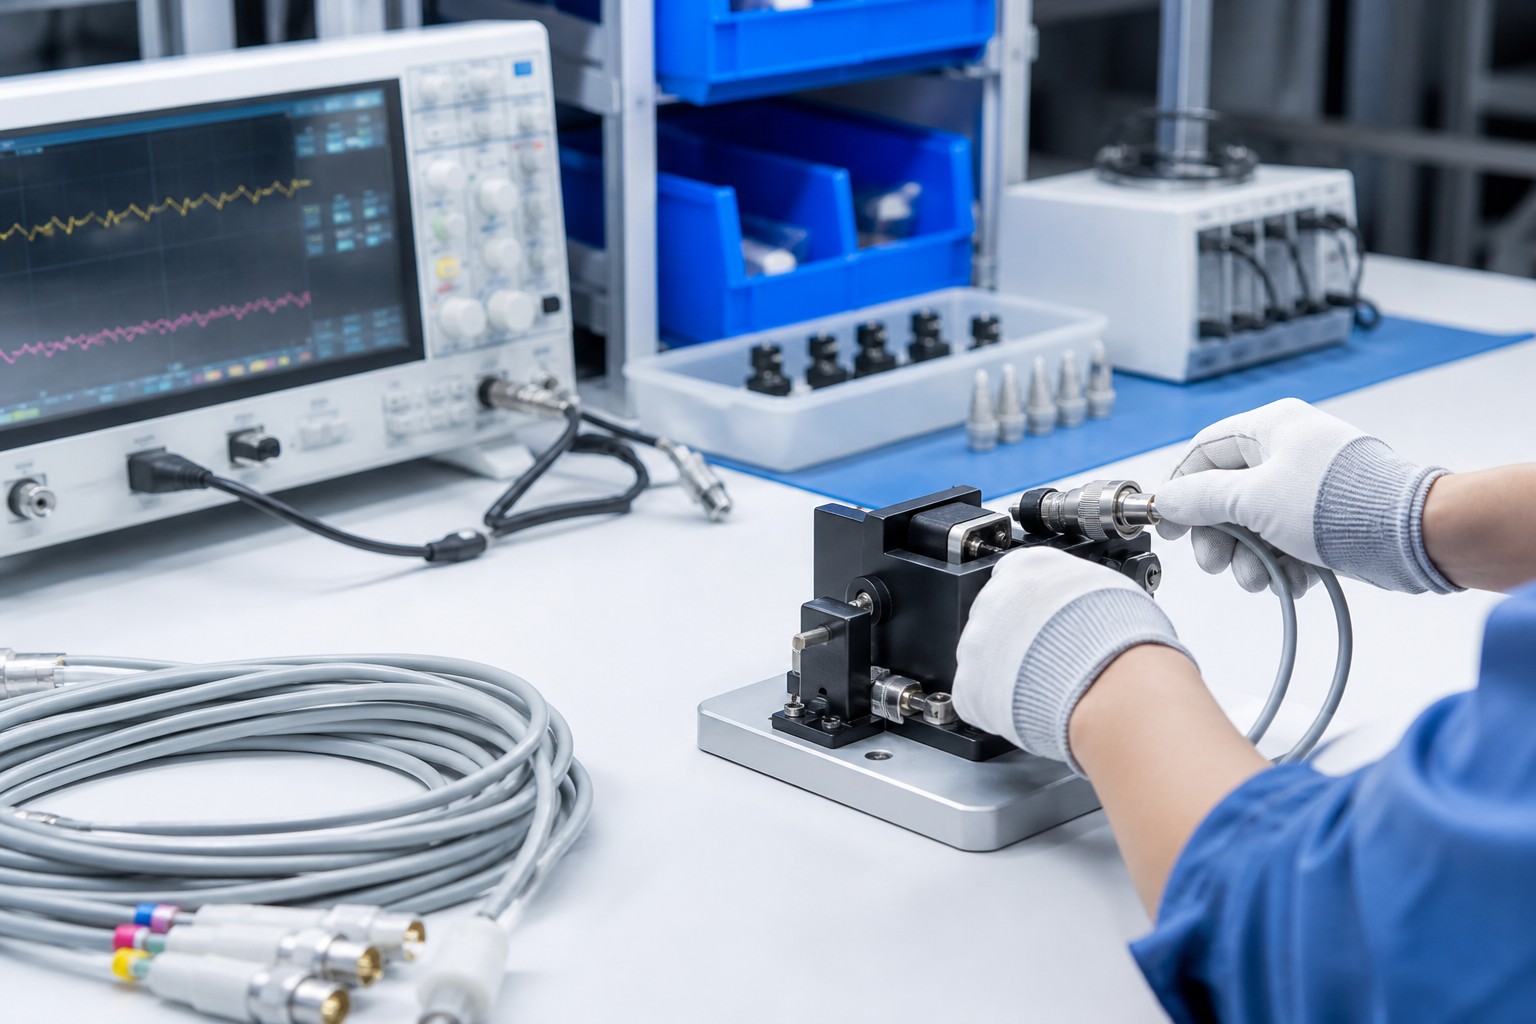
Quality Lab
Incoming & finished-goods inspection
Our Team
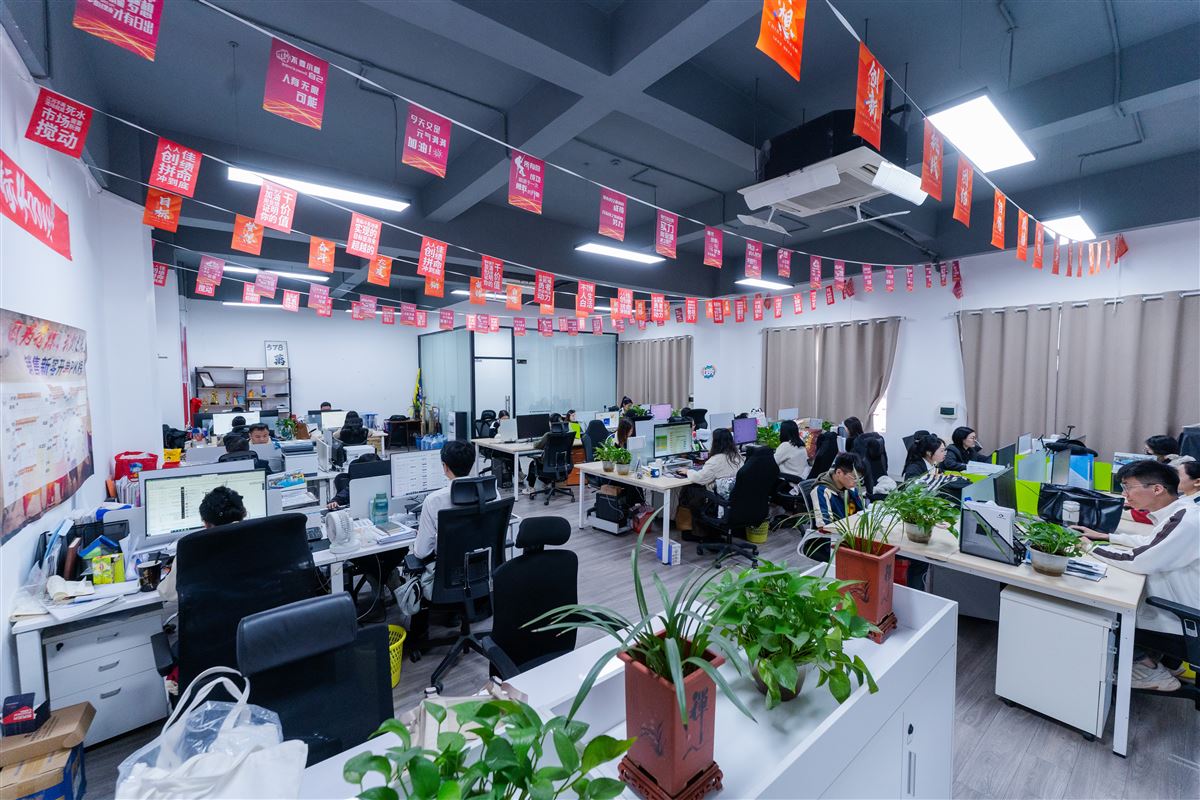
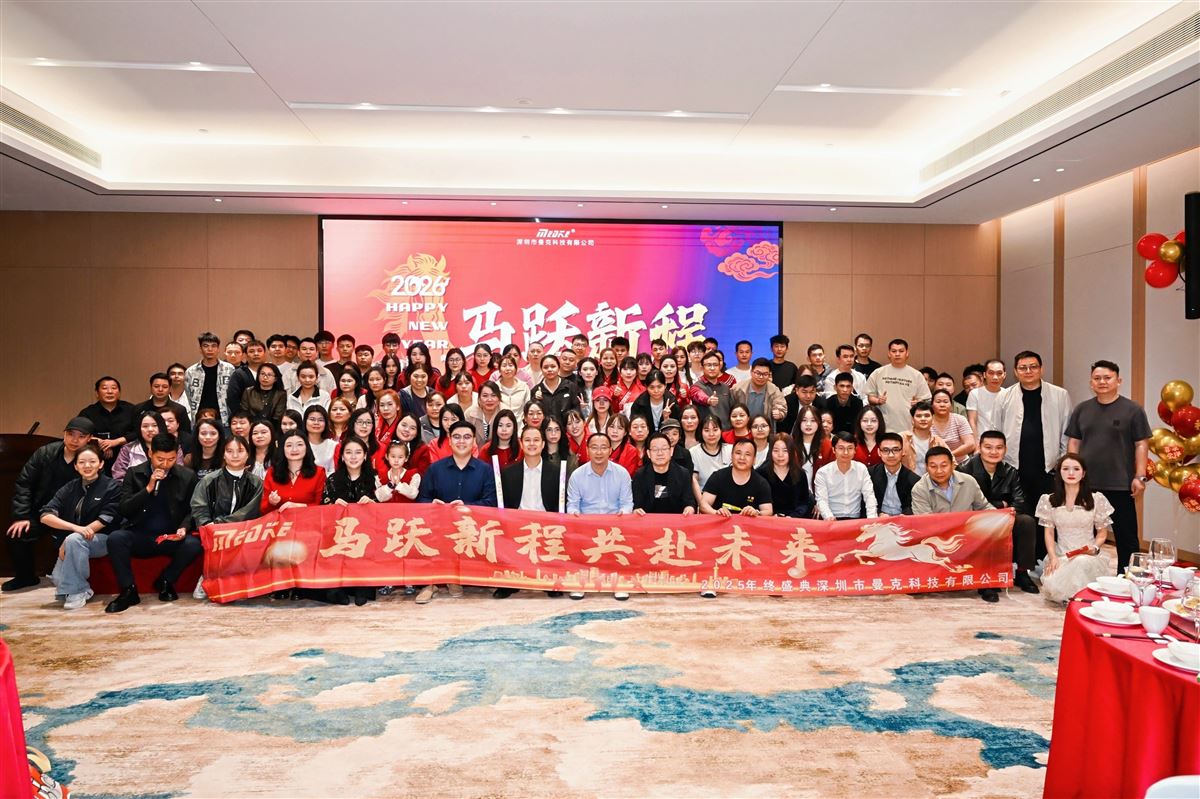
100+ professionals across sales, R&D and QC. Bilingual sales team replies within 24 hours; R&D supports custom connector and packaging development.
Our ISO 13485-certified plants run with full batch traceability, and a dedicated QC team covers incoming, in-process and finished-goods inspection on every order.